A fast-moving item can disappear from the warehouse long before anyone notices a spreadsheet needs updating. By the time a buyer raises an order, production may be waiting, sales staff may be promising stock that is not available, and finance is dealing with urgent freight costs. To automate stock replenishment properly, businesses need more than a low-stock alert. They need rules that reflect actual demand, supplier performance, production requirements and the stock already committed elsewhere.
For Australian manufacturers, wholesalers, retailers and processing businesses, replenishment automation is a practical control over cash, customer service and operational continuity. The objective is not to order more stock automatically at every opportunity. It is to place the right order, at the right time, for the right quantity, with clear approval and traceability.
Why manual replenishment creates expensive gaps
Many businesses start with a workable process: a storeperson checks bins, a planner reviews last month’s sales, and purchase orders are raised in response to experience. This can work while product ranges are small and demand is predictable. It becomes fragile as the business adds locations, suppliers, production stages, seasonal lines or customer-specific orders.
Manual review creates two common outcomes. The first is a stockout, where materials, spare parts or saleable goods are unavailable when needed. The second is excess stock, where working capital is tied up in slow-moving inventory that occupies warehouse space and may become obsolete.
The real issue is usually fragmented information. Sales forecasts might sit in one system, stock movements in another, production consumption on paper, and supplier lead times in a buyer’s inbox. A reorder point calculated from only one of these sources will be unreliable. Replenishment decisions need to draw from one current operational picture.
How to automate stock replenishment without losing control
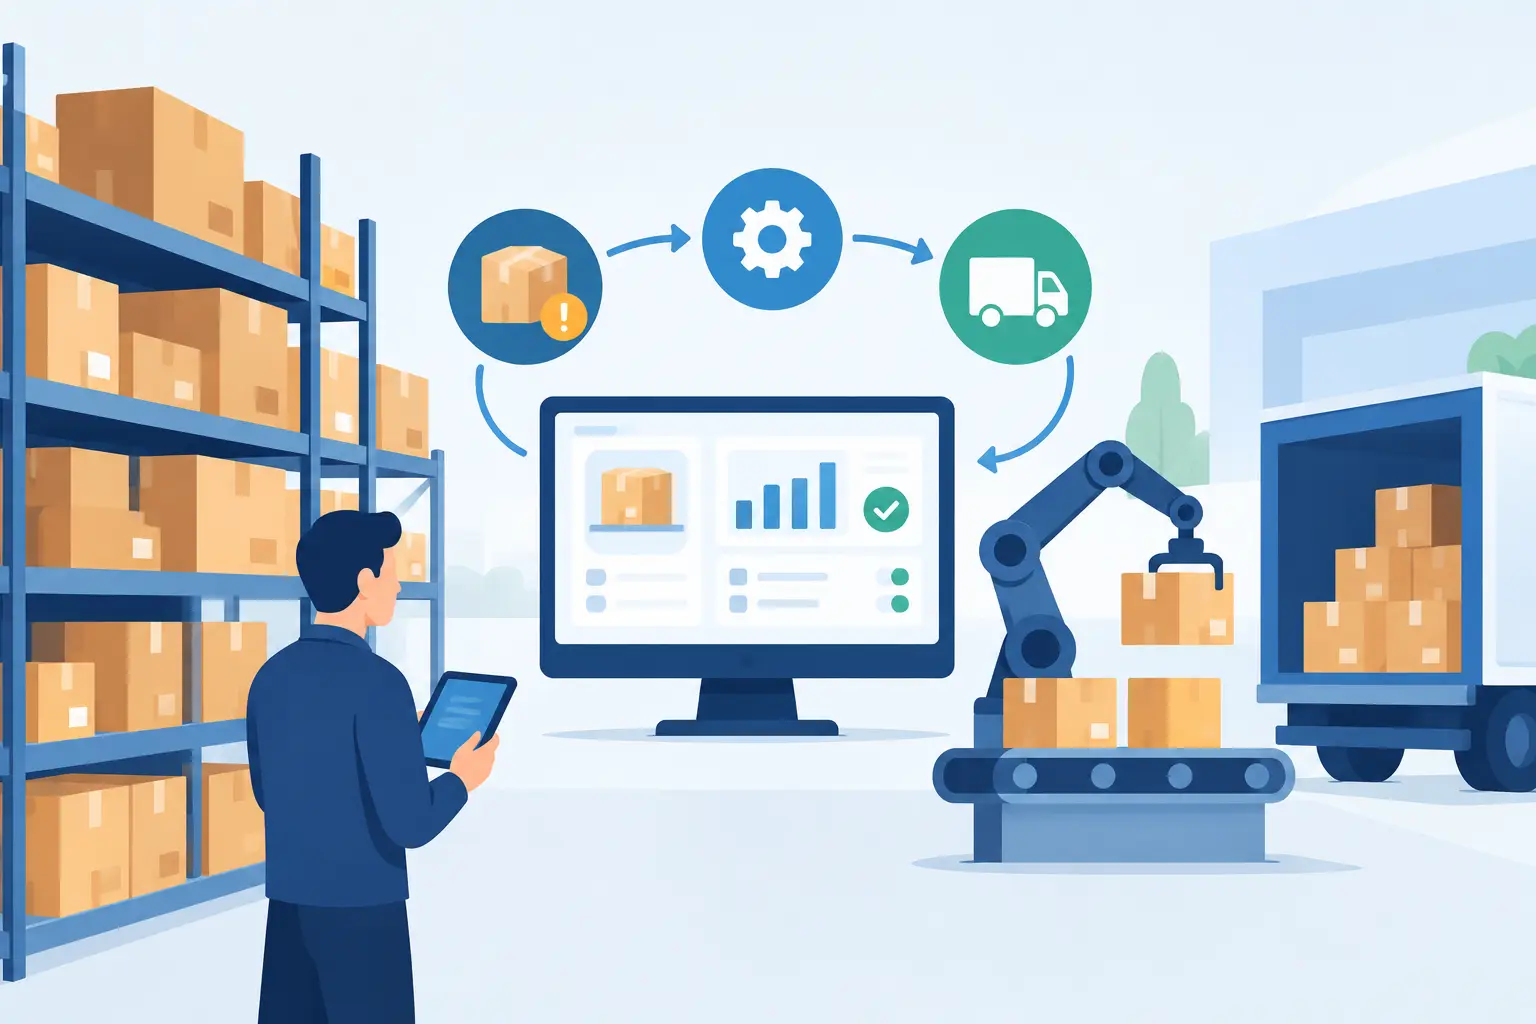
Effective automation begins with a clear inventory policy. The system can then monitor stock positions continuously, create replenishment suggestions or purchase orders when rules are met, and route exceptions to the right people. Automation handles repeatable decisions; people manage commercial judgement, unusual demand and supplier risk.
Start with clean, usable item data
No replenishment engine can compensate for inconsistent item records. Each stock item should have a standard unit of measure, accurate on-hand quantity, preferred supplier, typical lead time, purchase pack size and storage location. For manufacturers and processors, bills of materials, yield assumptions and expected wastage also need attention.
It is worth separating genuinely different items rather than grouping them under vague descriptions. A 10 mm fitting, for example, may look interchangeable with another fitting but have a different supplier, lead time or approved use. Clear item master data makes automated recommendations dependable and improves traceability during stocktakes and audits.
Accuracy also depends on disciplined transactions. Goods receipting, transfers, production consumption, returns and sales dispatch must be recorded when they occur. Barcode scanning, mobile warehouse processes and machine or PLC data can reduce delays and remove manual entry from high-volume operations.
Set replenishment rules that reflect real demand
A reorder point is commonly based on expected demand during supplier lead time, plus safety stock. If a business uses 40 units a week and its supplier generally takes three weeks to deliver, the minimum requirement is 120 units before allowing for variability. Safety stock protects against demand spikes, delivery delays and receiving discrepancies.
That basic formula is useful, but it should not be treated as permanent. Seasonal retail lines, plantation inputs, production chemicals and project materials often have different demand patterns. A fast-moving stock item may need dynamic rules based on recent sales and forecast demand, while a low-volume critical spare may need a fixed minimum because downtime costs more than carrying stock.
Order quantities matter just as much. Buying the exact shortfall can create too many small orders, while buying only in supplier carton quantities can overfill the warehouse. The right setting may be a minimum order quantity, a fixed order multiple, an economic quantity, or a planned quantity linked to the production schedule. It depends on storage capacity, freight thresholds, cash flow and supplier terms.
Include stock that is already committed or on the way
An available quantity is not always the same as the quantity physically in the warehouse. A dependable system considers on-hand stock, quantities allocated to customer orders, stock in quality inspection, transfer orders, incoming purchase orders and materials reserved for production.
This is where connected ERP workflows make a measurable difference. When a confirmed sales order reserves inventory, a work order consumes components, or a supplier delivery is receipted, the projected stock position updates immediately. The replenishment plan is based on what the business can actually use, not an out-of-date stock count.
For multi-site businesses, visibility should extend across warehouses, retail stores, workshops and third-party storage. Centralised visibility does not mean every location shares stock freely. It means planners can see where stock sits and apply transfer rules before placing another external order.
Automate recommendations first, then approvals
Businesses do not need to move straight from manual buying to fully automatic purchase orders. A sensible first step is to generate replenishment recommendations for buyer review. The buyer can assess suggested quantities, compare supplier prices, consolidate orders and adjust for known events such as a customer tender or planned shutdown.
Once confidence is established, low-risk items can be approved automatically within clear thresholds. Higher-value goods, volatile commodities and non-standard purchases can continue through an approval workflow. This approach protects spend control while removing repetitive checking from the purchasing team.
Approval rules should match the commercial risk. A routine order for standard packaging may only need the system’s policy checks. A large purchase of imported materials may require purchasing, operations and finance approval because currency movement, freight and holding costs all affect the decision.
Connect replenishment to production, sales and finance
Replenishment is not a warehouse-only process. In a manufacturing environment, demand can originate from sales orders, master production schedules, maintenance plans or machine data. A production plan should trigger requirements for raw materials and packaging early enough to protect the schedule, not after the line is waiting.
For process-based operations, the system may need to account for batch sizes, variable yields, expiry dates and quality holds. In hospitality and retail, replenishment may need to respond to daily sales, promotions, menu changes and location-level demand. Labour-hire and professional services businesses may have lighter stock requirements, yet still benefit from automated control of consumables, uniforms, equipment and job-specific materials.
Finance also needs a direct view of the outcome. Replenishment affects cash requirements, landed cost, gross margin and stock valuation. With purchasing, inventory and accounting in one platform, finance teams can see planned commitments before invoices arrive and investigate why stock investment is increasing. Power BI reporting can help leaders compare service levels, stock turns, supplier delivery performance and slow-moving inventory by location, product group or business unit.
Measure whether the rules are working
Automation should be reviewed as an operating process, not set once and forgotten. Track stockouts, emergency purchases, inventory turns, excess stock, forecast accuracy and supplier lead-time variance. If a product regularly runs out despite automated orders, the issue may be an incorrect lead time, underestimated demand, unrecorded allocations or a supplier that is no longer reliable.
Exception reporting is especially valuable. Planners should see items below safety stock, late purchase orders, unusual consumption, expiring inventory and recommendations affected by supplier minimums. This focuses attention where it is needed instead of asking staff to manually inspect every line every day.
A connected platform such as OneBusiness can bring inventory, purchasing, production, sales, financials and analytics into one workflow, while allowing replenishment rules to be configured around industry-specific operations. That is particularly useful where standard stock logic must work alongside batch production, machine data, multiple warehouses or specialised approval requirements.
Build automation in stages
The best implementation path is usually targeted rather than broad. Begin with high-volume, predictable items where data quality is strongest and the benefit is easy to measure. Validate the suggested orders against experienced buyer decisions, refine lead times and safety stock, then extend the model to more complex categories.
Keep a process for exceptions from the start. New products, supplier disruptions, major customer wins and seasonal demand shifts require human input. Good automation makes these exceptions visible early, with enough context for a planner to act decisively.
When replenishment is connected to the rest of the business, stock control becomes less about chasing shortages and more about planning with confidence. The result is a warehouse and purchasing function that supports growth without quietly absorbing more cash, more manual work and more operational risk.